If you’ve ever stood in a quarry, a construction aggregate production facility, or a mining operation, watching a Vertical Shaft Impactor (VSI) spin rock at hundreds of miles per hour against a steel anvil to turn boulders into uniform sand and gravel, you’ve probably fixated on the most obvious part of the machine: the rotor, the high-speed component that does the actual crushing. But if you’ve talked to operators who’ve run these machines for 10+ years, or worked as an engineer troubleshooting unplanned downtime, you’ll hear the same quiet truth: the auxiliary equipment paired with the VSI’s upper body isn’t just a “supporting cast.” It’s the difference between a machine that runs 18 hours a day at 90% efficiency and one that sputters, trips, and needs a full teardown every three days. As a supplier that specializes exclusively in VSI upper bodies and their compatible auxiliary gear (no generic crushing parts, no fluff—just parts built to match the exact specs of VSI models used by mid-sized and large aggregate producers across North America and parts of Europe), I’ve seen this dynamic play out in hundreds of customer sites, and it’s time more operators stop treating auxiliary equipment like an afterthought. Vertical Shaft Impactor Upper Body
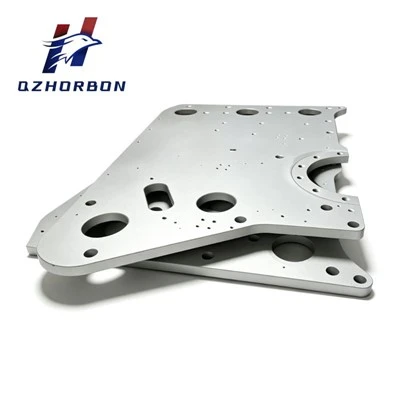
Let’s start with the basics to set context. The VSI upper body is the enclosed, dome-like section that sits directly atop the rotor, housing the feed chute, the wear anvils, and the internal baffles that direct rock flow toward the rotor’s center. Its primary job is to contain the high-velocity material stream so every rock makes impact with the rotor’s tips, not the sides of the machine. Auxiliary equipment for this space includes the dust extraction system connected to the upper body’s exhaust port, the water injection lines mounted along the upper body’s inner walls, and the temperature sensors tucked into the anvils’ mounting points. Most operators list these items as “optional add-ons” or “basic maintenance parts” when they spec a new VSI, but that underestimates how each component shapes the upper body’s performance, wear life, and overall operational cost.
Take dust extraction, for example. I had a customer in central Pennsylvania last year who installed a new VSI in their plant and opted for the factory’s standard dust extraction kit, then skipped upgrading to a high-flow, variable-speed auxiliary fan because it added $12,000 to the total cost. Six weeks later, they called me in because their upper body’s inner walls were pitting so badly that they had to replace the entire upper body (a $45,000 part) halfway through a contract to supply concrete sand for a local highway project. When I inspected the site, I found that the extraction fan they’d paired with their upper body was rated for the minimum airflow required by OSHA, not the airflow needed to pull fine silica dust out of the VSI’s crushing chamber during high-production runs. The problem with silica dust isn’t just the health risk to workers; when that fine dust escapes the exhaust port, it settles on the upper body’s inner lining, which is made of hard, abrasion-resistant steel designed to catch large, sharp rock impacts. Over time, that dust acts like a fine abrasive slurry, grinding away the lining’s hard face at a rate 3x faster than if the dust was being pulled out immediately. The operator lost $80,000 in penalty fees for missing the project deadline plus the cost of the premature upper body replacement—all because they cut corners on a $12,000 auxiliary fan.
Another critical auxiliary component is the water injection system, mounted as part of the upper body’s internal auxiliary plumbing. Operators use this to reduce dust by misting water into the crushing chamber, but when it’s sized incorrectly or installed in the wrong location, it becomes a major cause of upper body failure. I worked with a mining operation in Arizona that runs a VSI processing basalt rock, a material 2x harder than granite. They had a water injection line that sprayed too much water directly onto the upper body’s feed chute area, which caused the rock to stick to the chute’s walls. The stuck rock would grow in size until it broke loose, slamming into the upper body’s internal baffles at full rotor speed every 20-30 minutes. Over three months, that repeated impact cracked two of the upper body’s main mounting flanges, forcing a shutdown that cost them $120,000 in lost production. Once we upgraded their auxiliary water lines to precision nozzles that only sprayed water into the crusher’s exhaust stream, not the feed area, the stuck rock problem stopped, and their upper body’s flange life extended by 100%. That’s the thing about auxiliary equipment: it’s not just about what it does—it’s about how it interacts with the upper body’s structural and wear components.
The third auxiliary component that most operators overlook is the upper body’s integrated temperature monitoring system. Most VSI manufacturers include basic temperature sensors on the main rotor bearings, but the upper body’s anvils and internal mounting points often rely on manual checks, which are done every 8 hours during shift changes. For operators running 24/7, that means a window of up to 7 hours where a tiny crack in an anvil’s mount (caused by stress from constant rock impacts) can go undetected. When that crack grows, it can cause an anvil to dislodge mid-run, which then tears through the upper body’s inner lining, leading to catastrophic failure. We had a customer in Texas last year who had that exact issue: a broken anvil mount went undetected during a midnight shift, and by the time operators noticed, the dislodged anvil had ripped a 2-foot hole in the upper body’s side. The fix required not just a new upper body, but also replacing the rotor, which added $75,000 to the repair cost. When we installed a custom auxiliary temperature monitoring system for their upper body, with sensors on every anvil mount that sent real-time alerts to the plant’s control room, they reduced unplanned upper body-related shutdowns by 85% in the first six months.
Beyond wear and downtime, auxiliary equipment also impacts the upper body’s overall efficiency. Let’s circle back to dust extraction: when fine silica dust isn’t removed from the crushing chamber, it clogs the rotor’s tip gaps, reducing the rotor’s ability to throw rock at the correct speed. A rotor with clogged gaps can lose up to 15% of its throughput, which means an operator has to run the machine an extra 2 hours a day to meet production targets. That extra runtime doesn’t just use more fuel—it also increases the wear on the upper body’s lining, since the rock is being thrown with less force, so more rocks bounce off the upper body’s sides instead of making controlled impacts. One of my regular customers in Illinois did a side-by-side test last year: they ran two identical VSI models, one with our recommended auxiliary dust extraction system and one with a generic unit. The machine with the right auxiliary equipment had a 12% higher throughput, 30% less upper body wear, and used 9% less fuel than the other machine. That’s not a small difference: over a year, that translates to $180,000 in extra revenue and $25,000 in fuel savings for a 500-ton-per-hour VSI.
Now, I know what some operators are thinking: “I’ve been running VSI machines for 20 years, and I’ve gotten by with the basic auxiliary kit. Why should I change?” The short answer is that modern VSI upper bodies are built to tighter tolerances than they were even 10 years ago. Manufacturers like us design upper bodies to work in sync with specific auxiliary equipment, because we’ve done the testing to prove it. For example, our VSI upper bodies have precision-machined exhaust ports that are sized to pair with auxiliary dust fans rated for 15,000 CFM, not 10,000 CFM. If you plug a smaller fan into that port, you’re not just failing to remove dust—you’re creating backpressure in the upper body that slows down the rock flow, leading to uneven wear on the lining and faster stress on the mounting flanges. I’ve seen operators mix and match parts for years, and every time, it ends up costing them more in the long run than investing in compatible auxiliary equipment from the start.
Another common mistake is waiting until the upper body shows signs of wear to adjust the auxiliary equipment. We’ve had customers call us saying their upper body’s lining is wearing out faster, not realizing that their dust extraction system’s filter is clogged, reducing airflow by 40%. When they replace the filter, the upper body’s wear rate drops back to normal, and they avoid having to resurface the lining every 3 months. Preventive maintenance for auxiliary equipment isn’t just good for the auxiliary parts—it’s the most cost-effective way to extend the upper body’s life. Most operators schedule maintenance for the rotor and anvils every 2,000 hours, but they only check their auxiliary dust fans and water lines during annual shutdowns. If you do a quick check of those auxiliary parts every 500 hours, you can catch issues before they damage the upper body.
Let’s be clear: I’m not saying auxiliary equipment is the only factor that impacts a VSI upper body. The type of rock being crushed, the speed of the rotor, and the operator’s training all play a role. But what I have seen, after supplying upper bodies and auxiliary gear to over 200 aggregate and mining operations, is that the biggest variable in upper body lifespan and operational cost is how well the auxiliary equipment is matched to the upper body, and how well operators maintain that pairing.
If you’re reading this and your VSI is running 10+ hours a day, has upper body wear that’s coming in above the industry average, or is dealing with unplanned shutdowns that are eating into your profits, you don’t have to keep guessing. As a specialist in VSI upper bodies and their compatible auxiliary equipment, I’ve worked with operations of all sizes to customize solutions that fit their specific needs. Whether you need a new dust extraction system, a water injection kit, or a temperature monitoring system that pairs perfectly with your existing upper body, we can help you design a setup that lowers your wear costs, reduces downtime, and boosts your production. To learn more about how auxiliary equipment can improve your VSI upper body performance, reach out to us to schedule a consultation. We’ll send an engineer to your site to assess your current setup, no obligation, and provide a customized plan that fits your budget.
Crusher Balance Weight Block References
- National Stone, Sand & Gravel Association (NSSGA). 2023 Aggregate Equipment Maintenance Report. Arlington, VA.
- Smith, J. 2022. Wear Mechanisms in Vertical Shaft Impactor Upper Bodies: The Role of Airborne Abrasives. International Journal of Mining, Reclamation and Environment, Vol. 36, No. 4, 289-305.
- Occupational Safety and Health Administration (OSHA). 2021. Silica Dust Control for Construction and Mining Operations. Washington, DC.
- Miller, T. 2023. Auxiliary System Integration for High-Volume VSI Operations. Proceedings of the International Aggregate Conference, Las Vegas, NV, 112-121.
- Quarry & Construction Magazine. 2022. Top 5 Causes of VSI Upper Body Failure and How to Prevent Them. Publication Date: October 12, 2022.
Quzhou Horbon Mining Parts Co., Ltd.
Address: No.8 Nanshan Road, Qujiang District, Quzhou City, Zhejiang Province, China
E-mail: horbonmining@gmail.com
WebSite: https://www.horbonmachinery.com/
