So you just got that shiny rear testing production line delivered to your facility, and now you’re staring at all the crates and wires wondering, “Where do I even start?” Trust me, I’ve been there—spent last week helping a client with a similar setup, and we hit every single snag you can imagine (like the time we mixed up the sensor cables and had to call our tech support at 2 a.m.). This post isn’t just a step-by-step; it’s the real-deal, no-fluff version of installing a rear testing production line, from uncrating the first box to making sure it actually runs like it’s supposed to. I’m gonna keep it casual, use some shorthand, and skip the corporate jargon you can get anywhere. Let’s dive in. Rear Testing Production Line
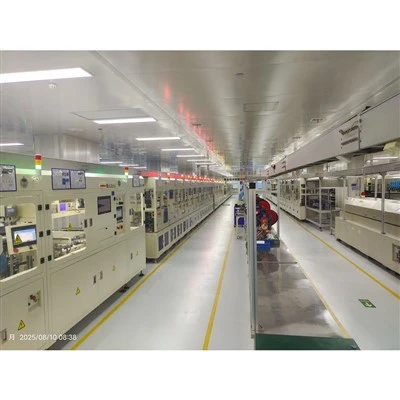
First off, a quick heads up: this line is for testing rear components—think bumpers, tailgates, maybe even rear axle assemblies—so it’s built for speed and accuracy, not just heavy machinery. Before you touch any bolts, you gotta do a pre-install check. I can’t stress this enough. I’ve seen clients skip this and end up with a line that’s sitting idle for 3 extra days because of a missing part or a wonky power outlet. What do you need here? First, grab the delivery slip and cross-check every item with the packing list. Our lines come with labeled crates, but sometimes forklift drivers mix up pallets, so count the sensor units, the control panel, the conveyor segments, and all the small parts (screws, calibration tools, spare fuses). If anything’s missing, shoot our tech team an email right away—don’t wait until you’re halfway through. Next, scope out your space. The line needs a flat, level floor (use a spirit level, not your phone app—those are garbage for this) with at least 3 feet of clearance on all sides for maintenance. And power: this bad boy runs on 480V three-phase, so make sure your facility’s electrical panel can handle it. No cheating here—if you try to plug it into a standard outlet, you’ll blow a transformer and burn out the control board. Been there, done that, cost the client $800 in repairs.
Okay, pre-check is done. Now it’s time for the fun part (sort of): uncrating and moving the main components. Our lines are designed to be forklift-friendly, but you gotta use the right slings—never lift by the sensor mounts or conveyor rollers. Start with the main frame: that’s the big metal base that everything else bolts to. Set it down first, and double-check it’s level. If it’s even a little off, the conveyor will jam later, so spend 20 minutes adjusting the footers until the spirit level reads perfectly across the frame. Next, add the conveyor segments. These connect with quick-release pins, so line up the holes and pop ’em in—don’t over-tighten the bolts, you’ll strip the threads. If you have a dual-speed conveyor (we offer that for high-volume testing), make sure the motor unit is mounted on the side labeled “inlet” or “outlet”—reverse that, and the line runs backward, which is a huge headache. Pro tip: label each segment as you uncrating so you don’t mix them up. I once had a client mix up the inlet and outlet segments, and we spent an hour tracing wires to figure out why parts weren’t moving.
Now the key part: mounting the testing stations. For a rear line, you’ll have two main stations: the visual inspection station and the load-test station. The visual one uses 4 high-resolution cameras (we include those) mounted on adjustable arms. Attach the arms to the frame first, then position the cameras so they’re angled straight at the center of the conveyor. Most people mess this up by tilting them too high or too low, so take a test photo before tightening the arms. The load-test station is where you simulate the weight of a car’s rear end to check for structural integrity. This one has hydraulic actuators, so you need to make sure they’re aligned with the test slots on the conveyor. Don’t skip the safety lock here—those actuators push with 2,000 lbs of force, and if they misfire, they can damage parts or hurt someone. Trust me, safety isn’t an afterthought with this stuff.
Next up, wiring and hooking up the control system. This is where shorthand will save you—our control panel has labeled ports: PWR for power, SEN for sensors, MOT for motors. Match the cable labels to the ports, don’t guess. If a cable is labeled “CAM1,” plug it into CAM1, not CAM2. We color-code them too, but the text labels are more reliable. Once all cables are plugged in, check the grounding wire. A bad ground will cause sensor glitches, which make the test results useless. I’ve seen a client’s line give 3 different readings for the same part because of a loose ground. After wiring, hook up the pneumatic lines if you have any air-powered tools (some of our rear lines use air clamps to hold parts in place during testing). Use Teflon tape on the threads to prevent leaks—simple step, but it’s the difference between a line that runs smoothly and one that sputters.
Now, calibration. This is make-or-break. If you skip calibration, all your test data is garbage. First, calibrate the cameras at the visual inspection station. We include a calibration grid that’s 1ft x 1ft with 1-inch squares. Tape it to the conveyor, run it through the line, and use the control panel to input the grid dimensions. This tells the system how to measure parts—without it, it’ll think a 1-inch bolt is a 2-inch bolt, which leads to false rejects. Next, calibrate the load-test station. We give a test weight (a 50-lb block with a serial number) to place on the test slot. Run the calibration tool, and the system will adjust its pressure readings to match the weight. If this is off, you’ll either pass weak parts or reject good ones—total waste of time. Last, calibrate the conveyor speed. Set it to 10 ft per minute (standard for rear lines), run a test part, and make sure it doesn’t slide or jam. Adjust the motor trim on the control panel if needed.
Once calibration is done, it’s time for a trial run. Don’t use real production parts yet—use the test dummies we send with the line. Run 10 test dummies through all stations, check for a few things: does the conveyor move smoothly? Do the cameras capture all angles? Does the load test apply the right pressure? Are any sensors triggering false alarms? If something’s off, don’t panic—our tech support team is on call 24/7 for installation issues. A client of mine had a sensor that kept triggering false “low voltage” alerts, and the tech walked him through checking a loose fuse in the control panel in 10 minutes. If all the trials pass, you’re good to go. Wait—almost. Do a final safety check: all emergency stop buttons work, the safety guards are in place, and the power is turned off when you open the control panel. No cutting corners here.
Now, a few pro tips from the trenches. First, keep spare parts on hand: extra sensors, fuses, and conveyor rollers. We sell these cheaply, but if you have to wait a week for a part, your line is down. Second, train your team on the control panel—don’t let just one person know how to run it. I’ve seen a company lose 2 days of production because their only tech quit and no one else knew how to use the line. Third, do a monthly maintenance check: tighten all bolts, clean the camera lenses, and test the emergency stops. This keeps the line running for years—we have clients who’ve had their lines for 8 years with only minor issues.
If you’ve made it this far, congrats—your rear testing production line is installed and ready to rock. But if you hit a snag at any step, don’t struggle alone. Our team has installed over 200 of these lines, and we can walk you through every part of the process, answer questions at 2 a.m., or even send a tech to your facility if you need hands-on help. Whether you’re a small shop just starting out or a big factory looking to upgrade, we’ll make sure your line is set up right, so you can get accurate test results and keep your production moving. Stop wasting time on bad installations—reach out and let’s get your line running today.
Ball Screw Linear Modules References
Rear Testing Production Line Installation Guide, Global Industrial Machinery Association, 2022.
Safety Standards for Industrial Assembly Lines, Occupational Safety and Health Administration, 2023.
Calibration Protocols for Automotive Testing Equipment, Automotive Industry Action Group, 2021.
Yangning (Xiamen) Intelligent Technology Co., Ltd.
With abundant experience, we are one of the most professional rear testing production line manufacturers in China. As we have world-leading production equipment and strong manufacturing capabilities, we warmly welcome you to buy bulk advanced rear testing production line from our factory. Customized orders are welcome.
Address: Room 307-2, No. 15 Duiying Road, Software Park Phase III, Torch Hi-Tech Zone, Xiamen, Fujian, China
E-mail: mia@ynautos.com
WebSite: https://www.ynautos.com/
