If you’ve ever stood on the assembly line of a heavy agricultural machine, watched a medical scanner rotate in sync with its patient, or felt the smooth glide of a precision robotic arm placing tiny components on a circuit board, you’ve used a special deep groove ball bearing. For over a decade, I’ve been a supplier of these critical parts, and I’ve lost count of how many times customers have asked me: “What makes your special deep groove ball bearings different from the off-the-shelf ones I can grab from a hardware store?” The short answer is the manufacturing process—one that demands precision, patience, and attention to even the most minuscule details that make the difference between a bearing that lasts three months and one that runs reliably for decades. Today, I want to pull back the curtain on exactly what goes into making a special deep groove ball bearing, from raw steel to the finished part that will keep your operation moving. Special Deep Groove Ball Bearings
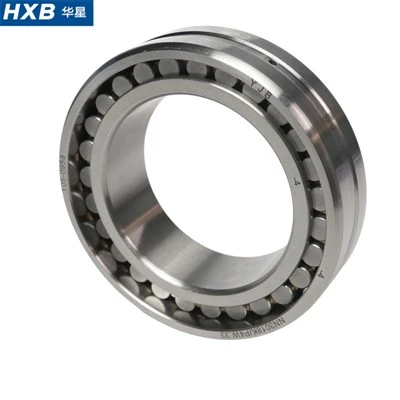
Let’s start with the raw material, because a bearing is only as good as the steel it’s made of. Most off-the-shelf ball bearings use standard carbon steel, but special deep groove ball bearings—designed for high speed, extreme load, low noise, or resistance to corrosion or high temperatures—need a material that can withstand whatever environment they’re thrown into. For our bearings, we use vacuum-degassed chrome steel (SAE 52100) for standard heavy-duty applications, high-nitrogen stainless steel (AISI 440C) for medical and food-grade equipment that needs to be sterilized repeatedly, and even heat-resistant tool steel for parts that operate in furnaces or aerospace systems. The steel arrives at our factory in large, solid bars, and the first step is not shaping it yet—it’s testing it. We take random samples from every batch to check for carbon content, inclusion levels, and hardness. A single tiny foreign particle trapped in the steel, smaller than a grain of sand, can cause a bearing to crack under load, so this quality check is non-negotiable. If a batch fails, it’s sent right back to the mill, no exceptions.
Once we confirm the steel is up to par, we move to forging. This is where the bearing’s rough shape starts to take form, and it’s a step that sets special bearings apart from mass-produced ones. For standard bearings, manufacturers often use cold heading, stamping steel into shape at room temperature, which is fast but leaves internal stresses that can weaken the part over time. For our special deep groove ball bearings, we use hot forging for all primary components: the inner ring, outer ring, and cage. We heat steel billets to around 1,200 degrees Celsius, hot enough to make it malleable but not so hot that it loses its molecular structure, then pound it in custom-designed dies that match the exact dimensions of our bearing models. Hot forging compacts the steel’s internal grain structure, making it stronger and more uniform than cold-formed parts. It’s also more work—each part takes about 10 seconds to forge, versus a fraction of a second for stamping—but the payoff is a bearing that can handle 20% more radial and thrust load than an equivalent cold-formed part. After forging, we rough-machine the rings to remove excess material, but we leave about 1-2 millimeters of extra material on each surface for later finishing. This leftover material gives us room to eliminate any defects from forging and refine the raceways—the curved grooves where the balls sit.
Next comes heat treatment, the most important step for a bearing’s hardness and durability. For special deep groove ball bearings, heat treatment isn’t a one-size-fits-all process. After rough machining, we harden the inner and outer rings by placing them in a controlled atmosphere furnace, heating them to 850 degrees Celsius for several hours, then quenching them in a slow-cooling oil bath. The slow cool prevents warping, a common issue with mass-produced bearings that can throw the raceway alignment off. Once quenched, we temper the rings at 180 degrees Celsius for another four hours to reduce brittleness—hard steel is strong, but it’s also prone to cracking if it hits a shock load, so tempering balances hardness and toughness. For our corrosion-resistant stainless steel bearings, we adjust the tempering process to prevent the steel from losing its rust-proof properties, a detail most small suppliers miss. After heat treatment, every ring is tested for hardness with a Rockwell C tester; any part that comes in at less than 58 HRC (our minimum requirement) is scrapped.
Now we move to the precision machining stage, where the bearing’s true accuracy takes shape. This is where we earn the “special” part of our deep groove ball bearings. Mass-produced bearings use high-speed lathes that cut multiple parts at once, but our special bearings are machined on CNC (Computer Numerical Control) lathes programmed to within 0.001 millimeters—less than the width of a human hair. First, we grind the back faces of the inner and outer rings flat, so they sit square in their housing. Then comes the most critical step: grinding the raceways. The raceway is the curved groove where the balls roll, and even a tiny imperfection here can create noise, generate heat, or cause premature wear. For standard bearings, raceways are ground with a simple wheel that cuts a basic curve, but for our special deep groove designs, we use form-ground raceways, where the grinding wheel is shaped to match the exact curvature we need, down to a tolerance of 0.0005 millimeters. This is what makes our bearings run smoother and quieter, even at 10,000 RPM or more. After rough grinding, we do a series of fine grinding and lapping passes, using a fine abrasive paste to polish the raceways to a mirror-like finish. The surface roughness of a standard bearing might be 0.2 microns, but our special bearings are finished to 0.05 microns—this reduces friction by up to 30% and extends service life dramatically.
Once the rings are ready, we move to the next core component: the balls. Special deep groove ball bearings use precision ground balls, not the stamped steel balls you might find in a toy. We source our balls from specialty manufacturers that produce them to AGMA (American Gear Manufacturers Association) Grade 10 or higher—this means they’re perfectly round within 0.001 millimeters, with no flat spots or surface imperfections. The balls go through their own series of processes: forging from the same steel as the rings, grinding, lapping, and polishing, then testing for roundness and size. For a typical 6205-size bearing, we use 13 balls, and we sort them into size groups within 0.0002 millimeters to ensure uniform load distribution across the raceways. Even a single ball that’s slightly smaller or larger than the rest can cause uneven wear and shorten the bearing’s life.
Now we get to assembling the bearing, and this is where the cage comes in—another detail that makes our special bearings stand out. The cage holds the balls in place, evenly spaced around the raceway, preventing them from rubbing against each other and causing friction and noise. Mass-produced bearings often use stamped steel cages, which are lightweight but prone to flexing at high speeds, leading to ball misalignment. For our special deep groove ball bearings, we use two types of cages depending on the application: pressed brass cages for heavy load applications, which are self-lubricating and durable, and high-performance polyamide cages for high-speed applications, which are lightweight and generate less heat at rotational speeds over 15,000 RPM. Assembly is done by hand by our skilled technicians, not by fully automated machines—automated assembly can miss small defects like a slightly misaligned ball or a tiny burr on the cage that causes noise. Each bearing is hand-assembled, with every ball carefully placed and spaced to ensure equal distance between them. Once assembled, we fill the bearing with a specialized lubricant tailored to the application: lithium-based grease for general use, food-grade NSF H1 grease for medical and food processing equipment, and high-temperature synthetic grease for parts operating at over 120 degrees Celsius. We don’t overfill the bearing—only 30% of the internal volume, because too much grease generates friction and heat, which can damage the bearing over time. After lubrication, we seal the bearing with either metal shields (for heavy load, dry applications) or rubber seals (for high contamination environments, like agricultural machinery, that keep out dust and water).
The final step before shipping is inspection and testing, the most important quality check of all. Every single one of our special deep groove ball bearings goes through a multi-point inspection, not just a random sample. First, we measure the dimensions of the inner and outer rings, the raceway curvature, and the ball sizes to ensure they meet our exact specifications. Next, we do a visual inspection under a microscope to check for any tiny burrs, scratches, or surface defects that would not be visible to the naked eye. Then we run performance tests: each bearing is mounted on a test rig and rotated at its maximum operating speed for 30 minutes, while we measure noise, temperature rise, and runout (how much the bearing wobbles as it spins). A bearing that produces more than 10 decibels of noise over our limit, or runs more than 20 degrees Celsius hotter than the setpoint, is rejected and taken apart to find the cause—whether it’s a misaligned raceway, a bad ball, or a lubricant issue. For bearings designed for corrosion resistance, we also perform a salt spray test, exposing them to salt water for 1000 hours to ensure they don’t rust. For bearings used in medical applications, we test the seals to make sure they can withstand repeated sterilization by autoclave without failing.
I know this sounds like a lot of steps, especially when you compare it to the process for a cheap bearing that costs a few dollars. But when you’re operating a robotic manufacturing line that runs 24/7, a wind turbine in a remote location that can’t be accessed for months, or a medical device that needs to work with perfect accuracy every time, that extra work pays off. A special deep groove ball bearing might cost 5 to 10 times more than an off-the-shelf part, but it will last 10 to 20 times longer, reducing downtime, maintenance costs, and the risk of expensive failures.
As a supplier, my job isn’t just to sell bearings—it’s to make sure you get the right bearing for your specific needs. Whether you’re looking for a bearing for a high-speed conveyor, a heavy-duty construction machine, a precision medical scanner, or a corrosive food processing line, we work with you to adjust every part of the manufacturing process: the type of steel, the cage material, the lubricant, the seal type, to meet your exact requirements. We don’t do one-size-fits-all, because we know that “special deep groove” means special to you.
If you’re tired of bearings that fail too soon, generate too much noise, or can’t handle the conditions your operation throws at them, I invite you to reach out for a procurement consultation. We can walk through your application, answer any questions you have about our manufacturing process, and help you find the right bearing that will keep your equipment running smoothly for years to come. Don’t settle for mass-produced parts that cut corners—choose a bearing that’s made with care, precision, and decades of experience.
High Speed Spindle Bearings References
- Harris, T.A., & Kotzalas, M.N. (2007). Rolling Bearing Analysis: Advanced Concepts of Bearing Technology. CRC Press.
- Bhadeshia, H.K.D.H. (2001). Steels for Bearings. Progress in Materials Science, 46(1-2), 1-230.
- American Gear Manufacturers Association. (2020). Standard for Ball Bearings (AGMA 9-B111).
- Todd, R.H., Allen, D.K., & Alting, L. (2012). Manufacturing Processes Reference Guide. Industrial Press Inc.
Hangzhou Huaxing Kechuang Holding Group Co., Ltd.
Hangzhou Huaxing Kechuang Holding Group Co., Ltd. is one of the leading manufacturers and suppliers of special deep groove ball bearings in China, featured by quality products and good service. Please rest assured to buy bulk durable special deep groove ball bearings from our factory. Welcome to view our website for more information.
Address: No.553 Yingbin Road, Linping, Hangzhou, 311100, China
E-mail: wmb@huaxingbearing.com
WebSite: https://www.hxbbearing.com/
